English
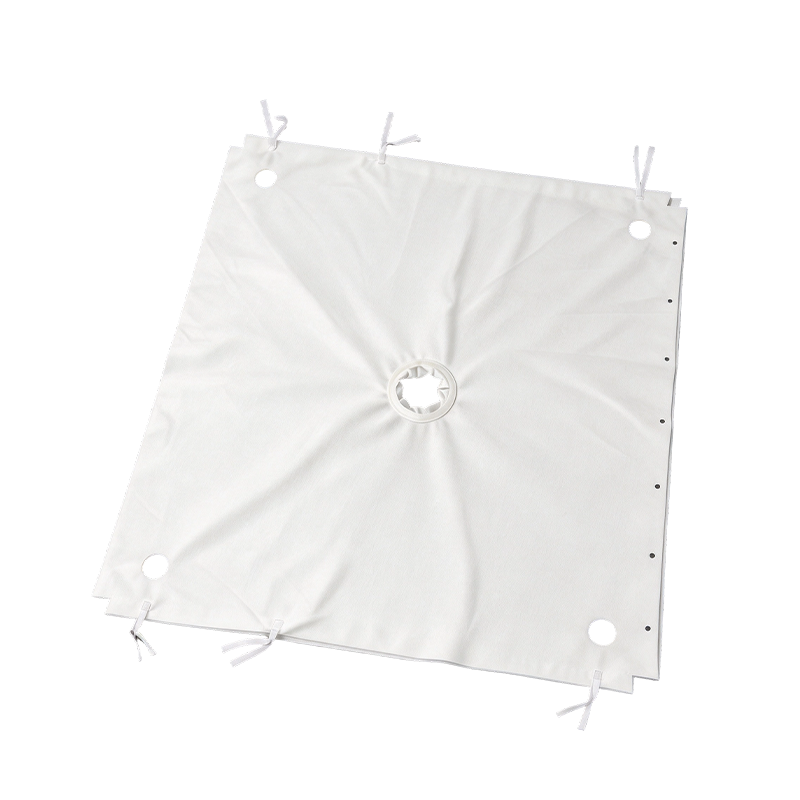
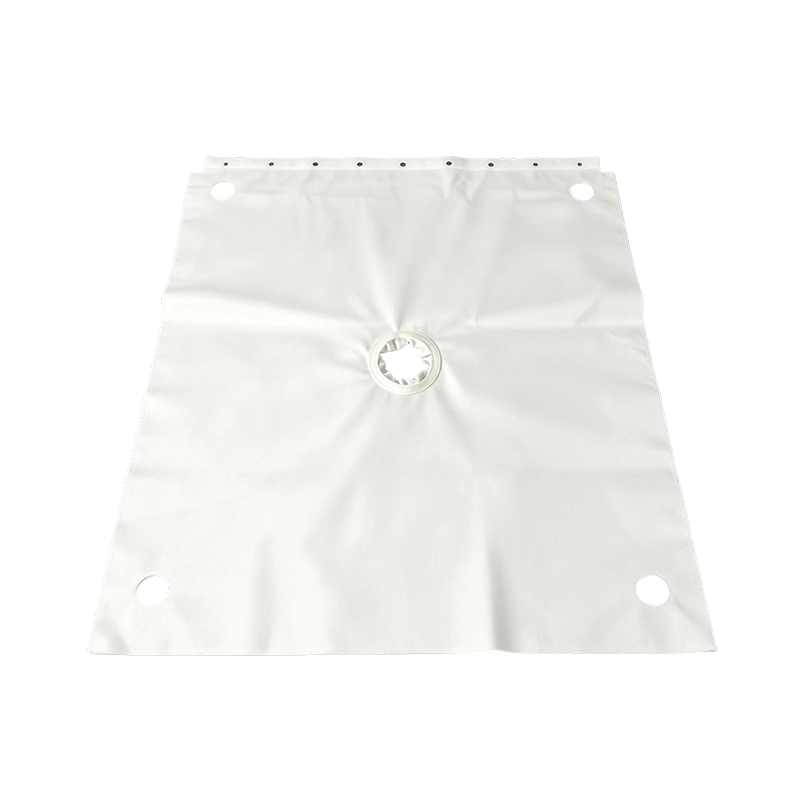
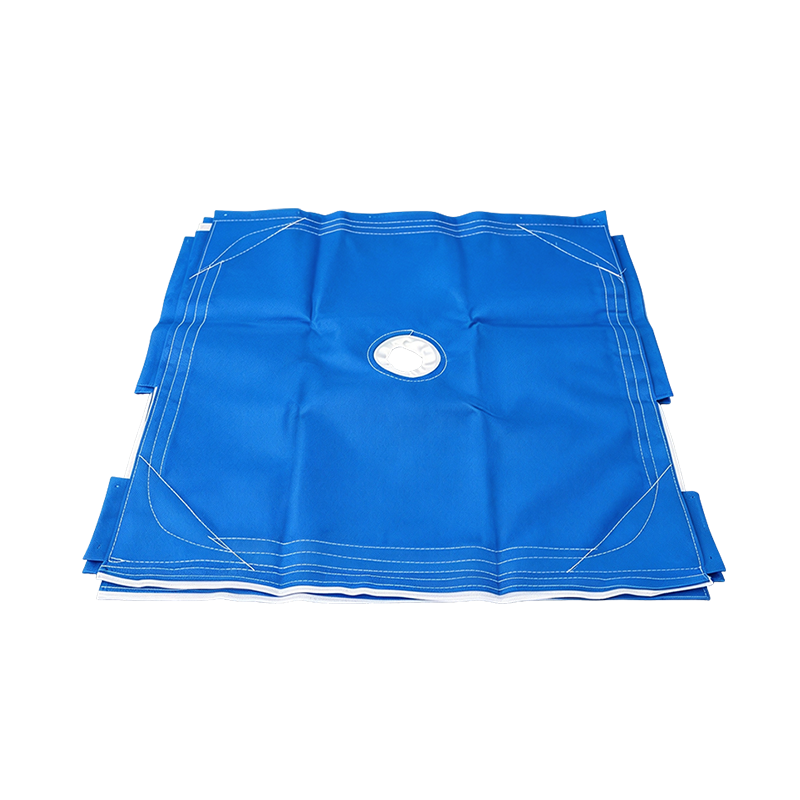
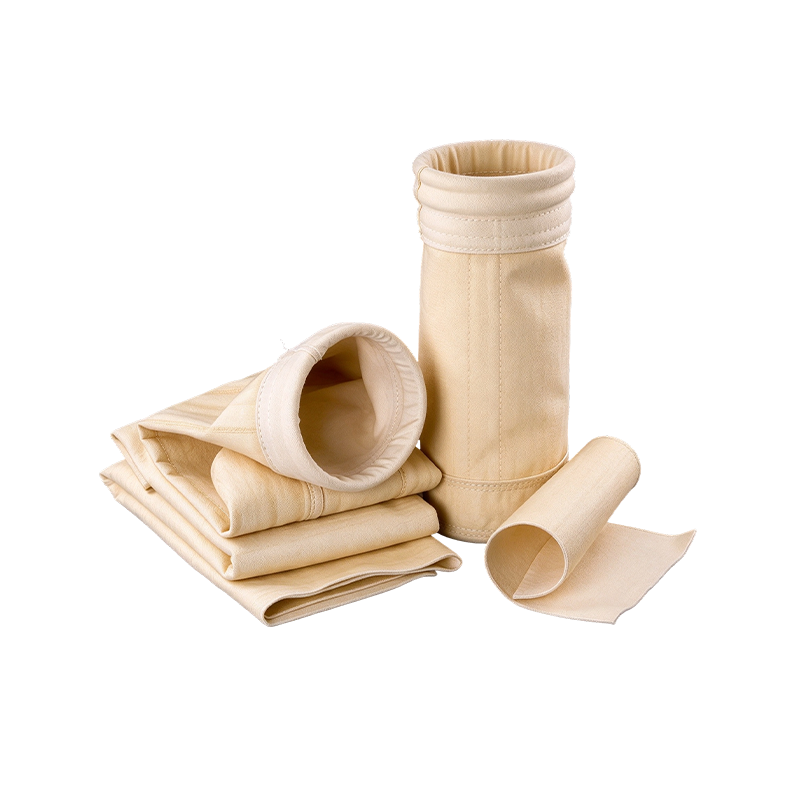
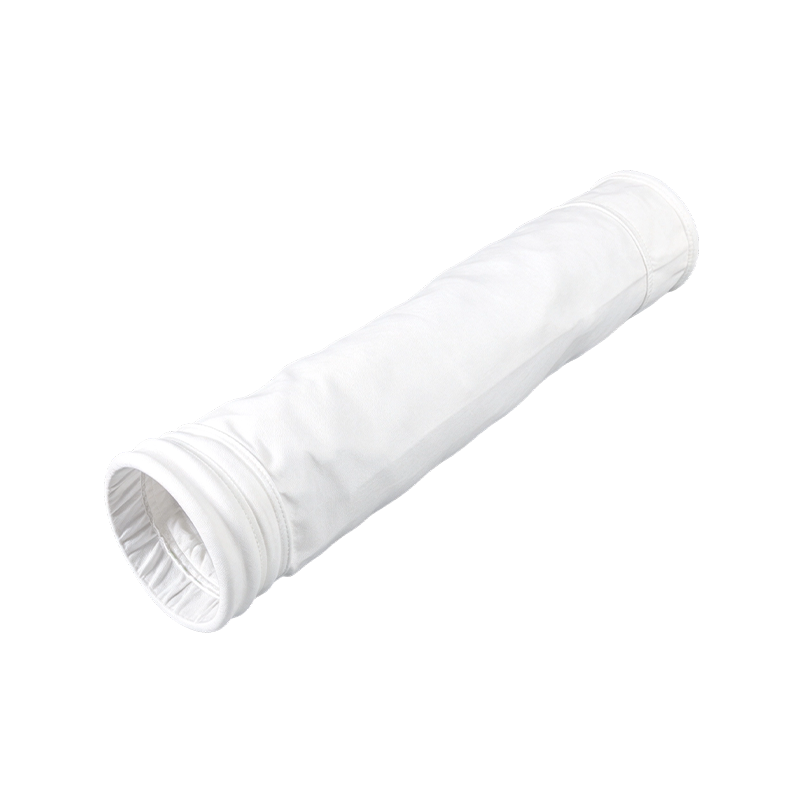
As global environmental and hazardous waste treatment standards for the chemical industry become increasingly stringent, chemical enterprises face higher filtration requirements in processes such as calcination, crystal slurry pressing, and sludge dewatering. Traditional filter cloth often suffers from short lifespan and easy damage when handling highly corrosive mother liquors and high-temperature materials, driving the growing market demand for high-performance industrial filter cloth.
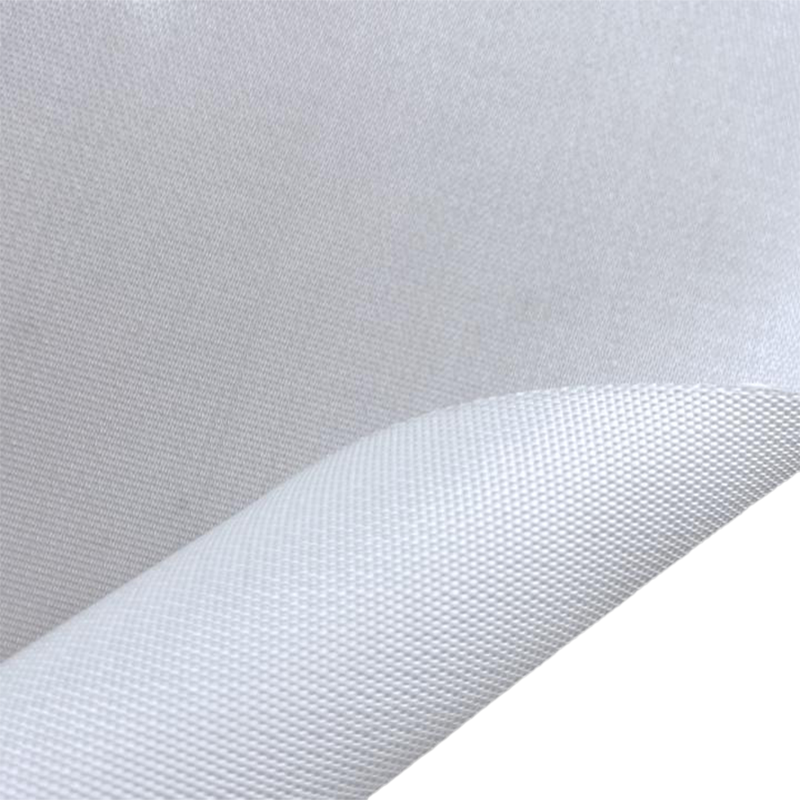
Industry analysis indicates that woven filter cloth featuring excellent chemical corrosion resistance, high tensile strength, and precise opening rates is becoming the preferred choice for chemical buyers. Furthermore, providing customized filter cloth selection and PTFE membrane treatment based on the characteristics of different materials—such as titanium dioxide, dyes, and inorganic salts—can effectively improve solid-liquid separation efficiency and reduce overall operational costs.